Top Moisture Analyzer Manufacturers for Global Buyers?

Time:2026-10-10 Author:Madeline
0%

Choosing the right moisture analyzer can shape product quality, production speed, and long-term testing costs. Global buyers often compare accuracy, heating technology, sample capacity, software, and service coverage. Yet a polished specification sheet does not always reflect daily laboratory performance.

This guide introduces leading moisture analyzer manufacturers serving international markets. It considers established expertise, documented calibration practices, application support, and equipment reliability. Some manufacturers focus on halogen heating for rapid routine testing. Others provide advanced systems for pharmaceuticals, food, chemicals, polymers, and research laboratories. Test conditions matter. A device that performs well with flour may require different settings for plastics or sludge.

Real experience should guide the purchase. Ask how samples are prepared, how results are verified, and whether local technicians can respond quickly. Review repeatability data, temperature control, weighing resolution, and data-export options. Check whether training, spare parts, and preventive maintenance are available in your region.

Small details matter.

No comparison is perfect. Published performance may change under different humidity, sample thickness, or operator habits. Buyers should test representative materials before approving a large order. Independent evaluations, recognized quality systems, transparent documentation, and customer references can strengthen confidence. This overview is designed to support careful decisions, not replace technical validation. The best manufacturer is rarely the one with the longest feature list. It is the partner that delivers dependable measurements, clear guidance, and consistent support after installation.
Top Moisture Analyzer Manufacturers for Global Buyers?

What Is a Moisture Analyzer and How Does It Work?

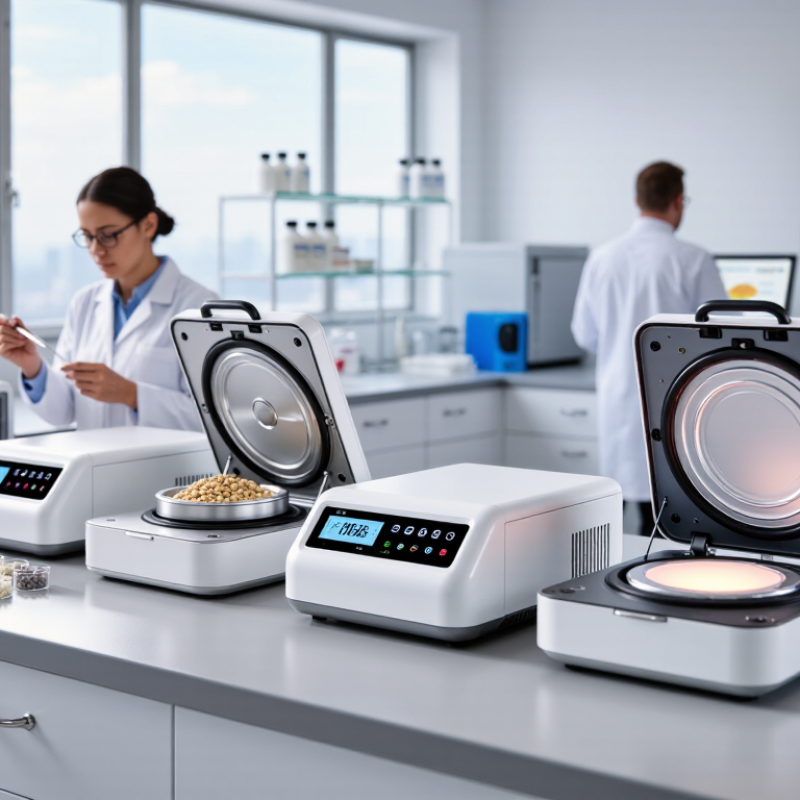
A moisture analyzer measures the water content in materials such as powders, grains, chemicals, and food ingredients. It combines a precision balance with controlled heating. The instrument records the sample’s starting weight, heats it, and measures weight loss during drying. The difference indicates moisture content. Many units use halogen or infrared heating for faster results. However, faster is not always better.

Reliable testing depends on sample preparation, temperature settings, and the stopping point. A thick sample may dry unevenly, while excessive heat can scorch it or remove other volatile substances. Experienced operators compare results with an approved reference method. They also check calibration with certified weights and keep clear test records. Small details matter. A cool draft can affect the balance.

Tips: Spread the sample into a thin, even layer. Use a consistent sample mass. Close the chamber before testing. Run duplicate tests when results seem unusual. Clean the pan after each session. If readings vary widely, review grinding, storage, and heating conditions before blaming the analyzer. Global buyers should also examine service support, training, spare parts, documentation, and measurement traceability. A low purchase price may hide slower support or difficult maintenance. Selecting a manufacturer requires more than comparing specifications. Ask for application data using materials similar to yours.

Key Factors for Comparing Moisture Analyzer Manufacturers

Comparing moisture analyzer manufacturers requires more than checking measurement speed or purchase price. Global buyers should examine practical performance under real operating conditions. Ask how the analyzer handles uneven samples, oily materials, or powders that clump during heating. A reliable manufacturer should provide repeatability data, temperature control details, and clear testing procedures. Look for instruments with traceable calibration options and documented methods.

Service quality often separates capable manufacturers from ordinary suppliers. Review warranty coverage, spare-part availability, software updates, and response times across your region. Technical support should explain sample preparation, not merely send a manual. Training records, validation guidance, and consistent documentation also show professional maturity. Independent test reports and customer references can strengthen confidence, especially when production decisions depend on small moisture differences.

Do not compare specifications alone. A faster result may be less useful if it damages the sample or produces unstable readings. Request a demonstration using your actual material, container, and target moisture range. Check whether the display remains readable beside a warm production line. Ask about cleaning after repeated tests. No comparison is perfect. Marketing language can sound precise while hiding method limitations. I would also record failed trials, not just successful ones. That small discipline often reveals more than a polished brochure.

Top Moisture Analyzer Manufacturers for Global Buyers

Key Factors for Comparing Moisture Analyzer Manufacturers

This illustrative 100-point procurement model highlights the factors global buyers commonly evaluate when comparing moisture analyzer manufacturers. Measurement accuracy and repeatability receive the highest weight, followed by temperature control, calibration support, service coverage, measurement speed, sample capacity, and data connectivity. The chart is a comparison framework rather than a ranking of individual companies or brands.

Leading Moisture Analyzer Manufacturers in Global Markets

Leading Moisture Analyzer Manufacturers in Global Markets

Leading moisture analyzer manufacturers now serve food, chemicals, pharmaceuticals, agriculture, and materials testing. Their strongest systems combine halogen or infrared heating with precise weighing and clear software. Global buyers should examine repeatability, drying-temperature control, sample capacity, and calibration support. A fast result is useful, but speed alone can mislead.

FAO’s 2019 report estimated that 14% of global food production was lost between harvest and retail. The UNEP Food Waste Index 2024 reported 1.05 billion tonnes of food waste in 2022. These figures do not measure analyzer demand. They do show why stable moisture control matters across storage, processing, and quality inspection. Leading manufacturers increasingly provide methods aligned with laboratory practices, including traceable calibration and loss-on-drying procedures. ISO/IEC 17025 remains a useful reference when buyers evaluate testing competence. Still, published specifications may not reflect dusty rooms, uneven samples, or rushed operators. That assumption needs checking.

Tips: Request application trials using your real material. Compare results with an oven reference method. Review service coverage, spare-part access, and training before purchase. Record sample mass, temperature, endpoint, and repeatability during trials. A perfect brochure is not evidence. Operator experience matters.

Top Moisture Analyzer Manufacturers for Global Buyers? - Leading Moisture Analyzer Manufacturers in Global Markets

Manufacturer Segment Common Global Markets Primary Heating Technology Typical Readability Typical Sample Capacity Typical Moisture Range Common Compliance Features Best-Fit Applications
Premium laboratory instrument manufacturers Europe, North America, East Asia, regulated laboratories Halogen or infrared heating with programmable temperature profiles 0.001 g to 0.0001 g; moisture display commonly 0.01% to 0.001% About 50–160 g Approximately 0.01%–100% moisture, depending on sample characteristics GLP/GMP documentation, calibration records, audit trails, method storage Pharmaceuticals, chemicals, food quality control, research laboratories
Industrial process-control manufacturers North America, Europe, China, India, Southeast Asia Halogen, infrared, or microwave-assisted systems 0.001 g to 0.01 g; moisture resolution commonly 0.01% About 35–200 g Approximately 0.1%–100% Method validation, password protection, data export, printer or network connectivity Production release testing, raw-material inspection, in-process control
Mid-range analytical equipment manufacturers Global distributors, academic laboratories, small and medium manufacturers Halogen or infrared heating 0.001 g to 0.01 g; moisture resolution commonly 0.01% About 50–120 g Approximately 0.1%–100% Digital temperature control, automatic endpoint detection, USB or serial output General food, feed, plastics, powders, textiles, and educational testing
Value-focused global OEM manufacturers Asia-Pacific, Latin America, Africa, price-sensitive laboratories Infrared or halogen heating 0.01 g; moisture resolution commonly 0.1% or 0.01% About 50–110 g Approximately 0.1%–100% Basic calibration, digital display, programmable drying temperature and time Routine incoming inspection, agricultural products, building materials, basic QC
Portable and field-testing manufacturers Agriculture, grain storage, construction, logistics, field service Capacitance, resistance, near-infrared, or microwave sensing Application-dependent; commonly displayed to 0.1% moisture Direct measurement; no laboratory sample pan required Often limited to a calibrated material-specific range Material calibration libraries, battery operation, automatic temperature compensation Grain, hay, wood, concrete, soil, paper, and on-site material screening
Specialized microwave moisture analyzer manufacturers Food processing, minerals, chemicals, biomass, continuous production Microwave energy with controlled sample heating Application-specific; laboratory units may reach 0.01% moisture resolution Typically 10–200 g for laboratory systems; continuous systems use flowing material Material-dependent; commonly used for low-to-high moisture products Process integration, alarms, analog or digital outputs, recipe management Rapid testing and continuous moisture monitoring in production lines
OEM and private-label system manufacturers Global distributors, laboratory-equipment integrators, contract suppliers Usually halogen, infrared, capacitance, or resistance sensing Commonly 0.001 g–0.01 g for laboratory units About 50–160 g for laboratory configurations Typically 0.1%–100%, depending on the sensing method Custom software, regional electrical standards, documentation and packaging options Distributor programs, customized laboratory packages, education and general testing

Specification ranges are representative of commonly available moisture-analyzer product classes in global markets. Actual performance depends on the instrument model, sample type, test method, calibration, and applicable standard.

How to Select the Right Manufacturer for Your Industry

Choosing the right moisture analyzer manufacturer requires more than comparing display size or purchase price. Match the instrument to your material, testing volume, and required accuracy. A food processor may need rapid halogen drying, while a pharmaceutical laboratory may require validated methods, sealed weighing chambers, and full audit trails.

Professional standards should guide the decision. USP <921> describes moisture determination requirements for pharmaceutical materials, while ISO/IEC 17025 emphasizes traceable calibration and competent testing. The FAO and WHO estimate that contaminated food causes about 600 million illnesses annually, showing why dependable moisture control matters. Ask manufacturers for repeatability data, certified reference materials, calibration records, and method-development support. A 2024 market analysis by Grand View Research also identifies quality control and process monitoring as major drivers of laboratory instrument demand. Market growth sounds impressive, but it does not prove technical suitability.

Tips: Request a sample test using your actual product. Check results across different moisture levels, not only one ideal batch. Confirm service response times, spare-part availability, software training, and local calibration support. Read the warranty carefully. A low initial price can become expensive when downtime interrupts production. I would also question unclear accuracy claims; “high precision” is incomplete without temperature range, sample size, and repeatability figures. Some selection mistakes remain invisible until an audit. That is the uncomfortable part.

Global Standards, Support Services, and Purchasing Considerations

Global buyers should evaluate moisture analyzer manufacturers through documented performance, not attractive specifications alone. A reliable supplier explains measurement principles, heating profiles, repeatability, and sample limitations. Ask whether results can support your existing laboratory procedures and quality system. Calibration should be traceable to recognized national or international standards, with clear uncertainty information. A certificate without traceability is not enough.

Support services often decide whether equipment remains useful after installation. Look for regional training, responsive technical assistance, spare parts availability, and practical maintenance instructions. Remote guidance can solve software issues quickly, but local service is valuable when sensors, heaters, or weighing systems fail. Language support matters too. So does response time.

Purchasing teams should compare total ownership costs. Include installation, calibration, consumables, shipping, import requirements, and staff training. Confirm voltage compatibility and environmental operating limits before ordering. Request application testing with your actual materials, especially powders, pastes, or heat-sensitive samples. Results can change with particle size and sample depth. Small details matter.

A strong manufacturer should also provide software records, audit trails, and data export options where regulated workflows require them. Yet no analyzer removes the need for trained operators. I have seen excellent instruments produce poor results after uneven sample spreading. The equipment may be advanced; the method may still be weak. Choose measurable support over confident promises, and record every assumption before purchase.

FAQS

What does a moisture analyzer measure?

It measures water content in powders, grains, chemicals, food ingredients, and similar materials. The sample loses weight during heating. That loss indicates moisture content.

How does a moisture analyzer work?

A precision balance records the sample’s starting weight. Controlled heating removes moisture. The instrument measures weight loss until the selected endpoint.

Why is sample preparation important?

Spread the material in a thin, even layer. Use a consistent sample mass each time. A thick sample may dry unevenly and produce unstable readings.

Can faster heating improve testing?

Not always. Excessive heat may scorch the sample or remove other volatile substances. A slower method can sometimes provide more trustworthy results.

What can cause inconsistent moisture readings?

Review sample grinding, storage, temperature, and heating conditions. A cool draft can disturb the balance. Clumped powders and oily materials may also dry unevenly.

How can operators improve measurement reliability?

Close the chamber before testing and clean the pan after each session. Check calibration with certified weights. Run duplicate tests when results look unusual. Small details matter.

What should buyers compare between moisture analyzer manufacturers?

Compare repeatability, temperature control, calibration options, service coverage, and spare-part access. Request trials using your actual material and target moisture range. A polished brochure proves little.

What records should a testing laboratory maintain?

Record sample mass, heating temperature, endpoint, results, and repeatability. Compare readings with an approved reference method. Keep failed trials too. They may reveal hidden method limits.

Conclusion

A moisture analyzer is a precision instrument used to determine the moisture content of materials by measuring weight changes during controlled heating. It is widely applied in food processing, pharmaceuticals, chemicals, agriculture, construction, and other industries where moisture levels affect quality, safety, consistency, and production efficiency. This article explains how the technology works and highlights key factors for comparing manufacturers, including measurement accuracy, heating methods, operating range, testing speed, software functions, durability, calibration options, and ease of maintenance.

It also provides guidance on evaluating leading moisture analyzer manufacturers in global markets without focusing on specific brands. Buyers will learn how to match equipment capabilities with industry requirements, sample types, testing volume, and regulatory expectations. In addition, the discussion covers international standards, documentation, technical training, warranty policies, after-sales support, spare parts availability, delivery terms, and total ownership costs. By considering both instrument performance and long-term service reliability, organizations can make a practical purchasing decision that supports stable quality control and efficient laboratory or production workflows.
Madeline

Madeline

Madeline is a dedicated marketing professional with a wealth of expertise in our company's core offerings. With a keen understanding of the industry, she brings a unique perspective to her role, consistently delivering high-quality content that highlights the superior aspects of our products. As......